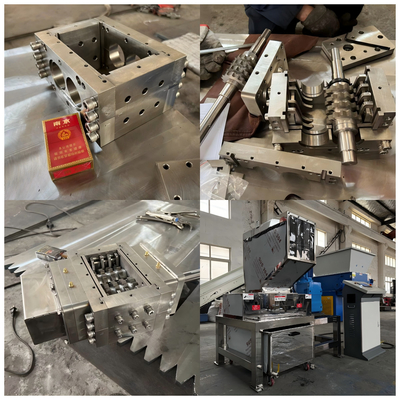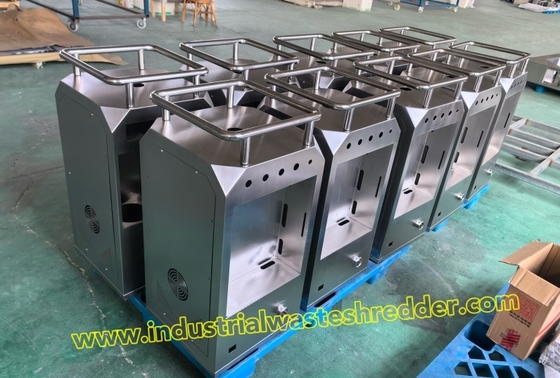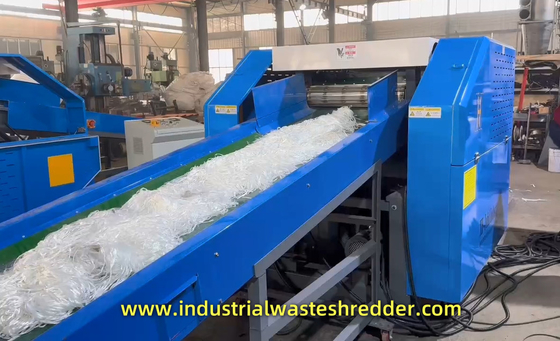
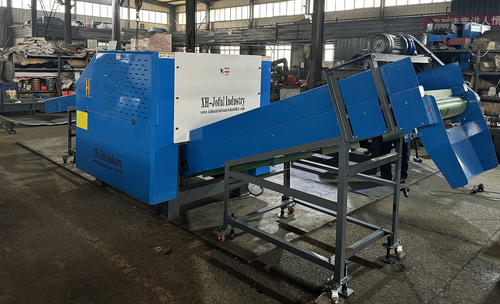
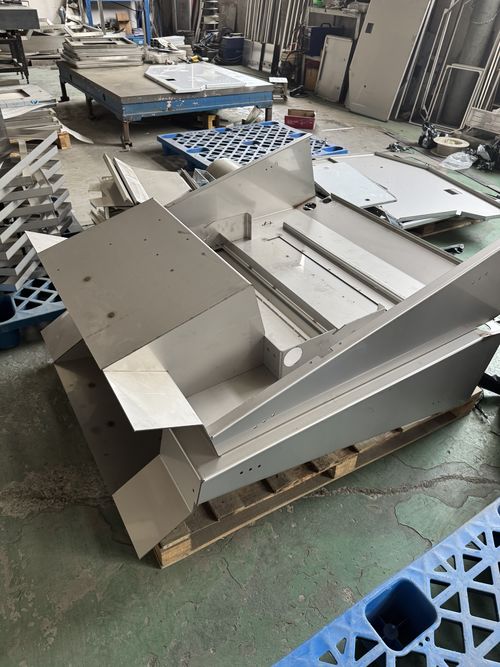
Project snapshot: a UK manufacturer of recycling and material sorting equipment needed a stainless steel fabrication partner for 316L hoppers, guards and control enclosures. Over 14 months the project moved from a single trial order to a quarterly release schedule, with lead time reduced by 35% and first-pass yield raised from 88% to 98.5%.
Client Background
ItemDetail
IndustryRecycling and material sorting equipment
LocationUnited Kingdom
Company sizeMid-sized OEM, 120 to 150 staff
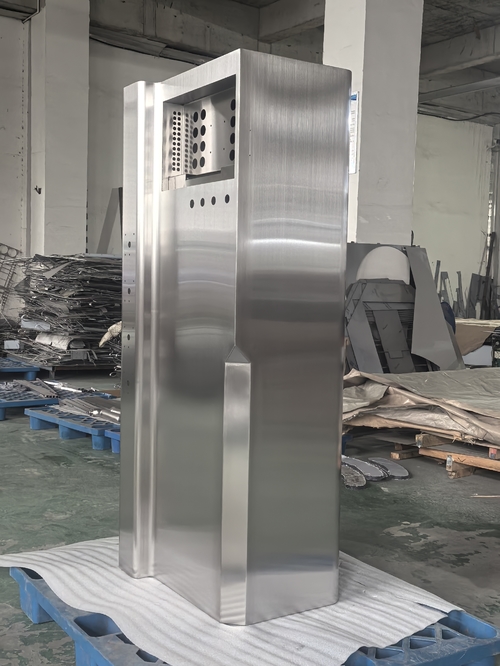
Parts in scope316L hoppers, side guards, control cabinets, mounting frames
Annual volumeAround 2400 fabricated assemblies
Service usedOEM sheet metal fabrication, welding, powder coating, kitting
The Problem
The client had been buying fabricated 316L parts from a local UK subcontractor. Three issues kept repeating. First, delivery slipped: quoted at 8 weeks, actual delivery ran to 12 weeks in peak season, which pushed machine assembly dates and forced expensive overtime. Second, weld quality was inconsistent. Hoppers that must hold liquid were failing leak tests on roughly one unit in eight, and rework had to be done after powder coating, which meant stripping, re-welding and recoating. Third, dimensional drift appeared on multi-part assemblies: brackets that passed inspection individually would not line up on the assembly line, because each part had been made from a different drawing revision.
Cost per part looked acceptable on paper, but the true cost including rework, line stoppage and air freight for urgent replacement parts was far higher than the purchase price suggested.
What We Changed
Drawing and revision control: one master drawing set was locked at project start, and every batch was produced against the same revision with a revision stamp on each part
Welding fixtures: jigs were built for the three highest-volume weldments so hoop distortion stayed within 1.5mm and leak tests became repeatable
First article approval: a full first article with CMM dimensional report and weld photographs was approved before any batch production
Material traceability: 316L mill certificates were filed per heat number and referenced on the packing list
Kitting: parts for one machine were packed and labelled as a kit rather than as bulk quantities, cutting line-side sorting time
Surface treatment: powder coating applied after all welding and leak testing, with 480-hour salt spray verification on test coupons
Execution Timeline
Week 1: drawing review, DFM report issued with 11 cost and quality suggestions
Week 2: quotation approved, NDA signed, welding jigs designed
Week 3 to 4: first articles produced and shipped by air for approval
Week 5: client engineering sign-off, minor bend radius change incorporated
Week 6 onwards: batch production in 3-week cycles, sea freight with 2 weeks buffer stock at client site
Results After 14 Months
MetricBeforeAfter
Average lead time12 weeks7.5 weeks
First-pass yield88%98.5%
Leak test failures per batch12 unitsFewer than 1 unit
Rework and recoating costBaselineDown 42%
Emergency air freight events5 per year0 in 14 months
Assembly fit-up complaintsRecurringNone since batch 2
Client Feedback
"The difference is predictability. We stopped building buffer stock to protect our assembly line, because the parts arrive when promised and they fit the first time," said the client's purchasing manager. "The DFM notes in the first quote paid for themselves in the first three batches."
Why The Project Worked
Three things made the difference: fixtures instead of skill-dependent welding, one locked drawing revision across every batch, and inspection data shipped with the parts so the client could verify rather than guess, and a single English speaking engineer accountable for the account.
Similar Project?
We fabricate 304 and 316L parts for recycling equipment, food machinery, medical housings and water treatment systems. Send your drawing with material, thickness, finish and annual quantity, and our engineering team will reply with a costed quotation and DFM notes within 12 working hours.
Çözümlerimiz. Çözümlerimiz
✨ Müşterilerin hassasiyet, kalite ve teslimat alanındaki zorlukları çözmelerine yardımcı olmak için sonundan sonuna kadar paslanmaz çelik metal tabakası imalat hizmetleri sunuyoruz.
✅ Anahtar Çözümler
Özel Üretim.Çizimler veya örnekler temelinde yapılan paslanmaz çelik metal parçaları.Çizimlere veya numunelere göre yapılmış, çelik ve altın parçaları.
Kesinlik ve Kalite KontrolüKatı tolerans yönetimi ve nakliye öncesi %100 denetim.Gömülmeden önce %100 denetim.
Esnek ÜretimPrototiplerden büyük ölçekli siparişlere kadar, ihtiyaçlarınıza uyarlıyoruz.Küçük ve büyük seri üretimleri de desteklenir.
Hızlı teslimat süresi.Acil programları karşılamak için hızlı prototip ve verimli üretim.Hızlı, verimli üretim, acil teslimat süresi.
Tek Duraklı Hizmet.Tasarım desteği, lazer kesimi, bükme, kaynak, yüzey işleme ve montaj.提供设计支持,激光切割,折??,接,表面处理到总装配的全过程服务.
Profesyonel bir paslanmaz çelik sac metal imalatçısı olarak, özelleştirilmiş ekipman muhafazaları için uçtan uca işleme hizmetleri sunmaktayız. Ham sac malzemeden tamamen monte edilmiş ve bitmiş bir ürüne kadar, her adım uluslararası kalite standartlarını karşılamak üzere hassasiyetle tamamlanır. Aşağıda, paslanmaz çelik ekipman muhafazaları üretimi için tipik iş akışı bulunmaktadır:
1. Malzeme Seçimi ve Kesim
Yüksek kaliteli paslanmaz çelik saclar (SS304 veya SS316 gibi) seçerek başlıyoruz. Müşterinin çizimlerine göre, malzemeler hassas ölçüler ve temiz kenarlar elde etmek için lazer kesim, CNC giyotin kesim veya zımbalama kullanılarak işlenir.
2. Bükme ve Şekillendirme
Kesilen parçalar, hassas bükme açıları ve tutarlı tolerans kontrolü sağlamak için CNC abkant presler kullanılarak şekillendirilir. Çok adımlı bükme veya haddeleme işlemleriyle karmaşık şekiller elde edilebilir.
3. CNC İşleme ve İkincil İşlemler
Daha yüksek hassasiyet veya özel özellikler gerektiren bileşenler için, detaylı fonksiyonel gereksinimleri karşılamak üzere CNC frezeleme, diş açma, havşa açma ve delme işlemleri gerçekleştiriyoruz.
4. Kaynak ve Montaj
Yapısal ihtiyaçlara göre parçaları birleştirmek için TIG kaynağı, MIG kaynağı, nokta kaynağı veya saplama kaynağı kullanıyoruz. Kaynak işleminden sonra, parçalar uyumu ve kararlılığı doğrulamak için monte edilir.
5. Yüzey İşlemi
Görünümü ve dayanıklılığı artırmak için aşağıdakiler dahil olmak üzere çoklu bitirme seçenekleri sunuyoruz:
Taşlama ve parlatma
Fırçalama
Kumlama
Pasivasyon veya parmak izi önleyici kaplama
Bu işlemler korozyon direncini artırır ve istenen görsel etkiyi sağlar.
6. Kalite Kontrol
Her parça, sıkı boyut kontrolünden, kaynak kalitesi kontrollerinden ve fonksiyonel testlerden geçer. Kalite ekibimiz, tüm bileşenlerin ambalajlamadan önce müşteri spesifikasyonlarını ve uluslararası standartları karşıladığından emin olur.
7. Son Ambalajlama ve Sevkiyat
Bitmiş muhafazalar temizlenir, film/köpük ile korunur ve küresel müşterilere güvenli teslimat sağlamak için ihracat için güvenli bir şekilde paketlenir.